In this guide
- Write a scope that follows the product risks
- Insert hold points before concealment
- Make findings actionable and bounded
- Use the inspection result in shipping and handover
- Use a failed sample to check the inspection rule
- Test the physical and commercial chain together
- Specify independent evidence without overclaiming it
- Translate the decision into a comparable request for quotation
- Plan evidence, interfaces and the final handover
- A commercial release gate for this order
- Illustrative project exercise
- Conclusion
Procurement guidance by the HabKube project team. Examples and AI-generated images are illustrative, not documented customer deliveries or certified test results. Confirm technical and statutory requirements with qualified destination professionals.
Write a scope that follows the product risks
What a buyer should document
Start with the approved product and inspection documents: drawings, bill of materials, agreed tolerances, component evidence and relevant test methods. Identify the critical-to-use items, not just easily visible finishes. For one project that may be intermodule connections; for another, wet-area joints or shipping protection. Distinguish 100% checks, sampling and document review. If sampling is used, agree how samples are chosen and what happens when one fails. A vague instruction to “check quality” leaves too much to the inspector’s discretion.
State whether the inspector is witnessing factory tests, checking records, measuring the supplied units or attending the final load. These are different assignments and may require different equipment or access. Ask the inspection company about competence for the technical scope and conflicts of interest. Decide who provides calibrated instruments, safe access and translated documents. Schedule the visit with enough notice that the required work will be visible.
Insert hold points before concealment
What a buyer should document
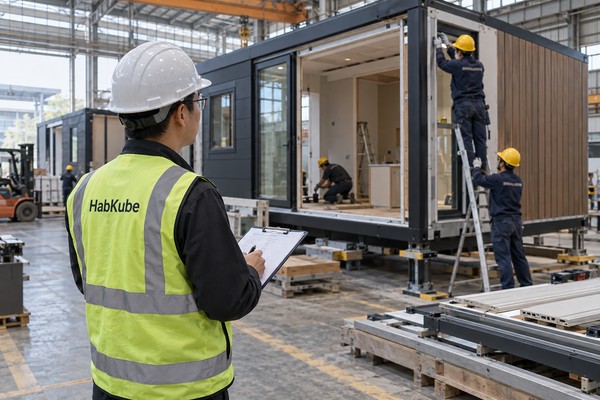
Some evidence disappears after cladding or interior finishes close. Put hold points at material receipt, frame fabrication, services rough-in, representative joint assembly and final packaging as relevant. Not every order needs the same number of visits, but a single pre-shipment inspection cannot see every hidden connection. The buyer should review cost and risk to decide where independent observation adds value. The supplier’s own quality-control records continue through production; an outside inspector samples or witnesses them, not replaces them.
Agree what constitutes a hold, a witness and a document review. A hold point means work should not proceed until the named party releases it under the contract. A witness point lets an invited party observe a planned activity; its effect if absent must be agreed. Clear definitions prevent a late dispute where one team assumes the inspector had approval authority and another assumes the visit was advisory only.
Make findings actionable and bounded
What a buyer should document
The report should identify unit, lot, location, drawing revision, observation, acceptance reference, severity and proposed next action. Photographs need captions and scale where useful. A note such as “paint poor” does not show whether an acceptance criterion was breached. If a dimension fails, report measured value, specified value and method. If testing is outside scope, say so. A credible report separates facts, exceptions and recommendations rather than turning uncertainty into a pass.
Define a corrective action loop. The supplier responds with cause, correction and evidence; the buyer or inspector reviews it under the agreed authority. A defect may need reinspection, a document revision or a destination engineering decision. Agree which unresolved items can remain on a punch list and which block shipment. For design deviations, an independent inspector should not approve a substitute structural member merely because it appears strong. Refer it to the design approver.
Use the inspection result in shipping and handover
What a buyer should document
After technical release, confirm packing-list accuracy and protection for transport. A complete physical unit can still ship without installation hardware, seals or manuals. The inspector can reconcile package IDs and quantities if the assignment includes loading. Record any condition that changes during loading and who assumes custody afterward. Keep the final report with photographs, corrective-action closeout and approved documents in the receiving pack.
At the destination, inspect for transit damage separately. Do not blame the factory inspector for a dent that occurred later, and do not use the lack of transit damage to dismiss a hidden factory defect. The independent report is one part of an evidence chain from design through site acceptance. When buying multiple phases, review findings across the first batch and update the inspection plan for later production. That learning is more valuable than repeating an unchanged checklist on every order.
Use a failed sample to check the inspection rule
A practical exercise before order release
Write a sample case before the inspector arrives: one fastener pattern differs from the approved drawing in a chosen module. The inspector records location, revision, measured observation and specified requirement. What happens next? Does the supplier correct only the observed area, inspect the rest of the lot, or seek a design concession? The answer depends on the contract and technical significance, not the inspector’s mood. Specify the escalation path and who can authorize a deviation.
Try a second case in which the factory presents a newer drawing than the buyer approved. The inspector should not simply compare the product to the newest paper on the table. It needs a controlled revision register and evidence that the buyer or designated designer accepted the change. If the change is legitimate, update the inspection basis. If not, record the mismatch. This matters especially for custom units with multiple room types or phased shipments, where a detail can be correct for one batch and wrong for another.
Finally, rehearse report closeout. The supplier submits correction photos, but the inspector’s original concern involved a concealed connection. Decide whether new photos, a reopened assembly or another witness visit is needed. Document that decision with the person who made it. The purpose of independent inspection is not to produce a glossy pass document; it is to give purchasing a reliable, bounded record for release and later receiving.
Test the physical and commercial chain together
An implementation check for the buyer
A sound procurement decision must survive the handoff from contract to factory to freight to site. Put the product IDs, quantities, controlled drawings and agreed deliverables on one schedule. Then ask where those identifiers appear in inspection and shipping documents. If a change is approved halfway through production, the old and new versions must be distinguishable. An unlabeled stack of components can be technically correct yet difficult to receive or assemble. Link milestones to records that the buyer can actually inspect.
Check that the delivery term and payment terms answer different questions. One allocates certain transport obligations and risk at a named point; the other states when money is due and against which evidence. Neither by itself specifies import permissions, local unloading or the authority to occupy. Use a responsibility matrix rather than one phrase such as “delivered and installed” unless every included task is defined. For an overseas project, ask the carrier, broker and destination team to confirm their assumptions before the factory locks packaging and dispatch date.
Build a conservative schedule around dependencies rather than an ideal dispatch day. Design approval, any specialist test, independent inspection, booking, customs documents and site readiness may run in parallel only where information is available. Identify a decision gate before a late change would require repacking or rework. If a milestone slips, agree how the buyer and supplier will update the production and freight plan. A transparent revised forecast is more useful than repeated unsupported promises that the original date still holds.
Project brief
Write the inspector’s scope before production
Share drawings, quality priorities and expected shipment date with HabKube so factory hold points can be discussed before access is lost.
Get a project quote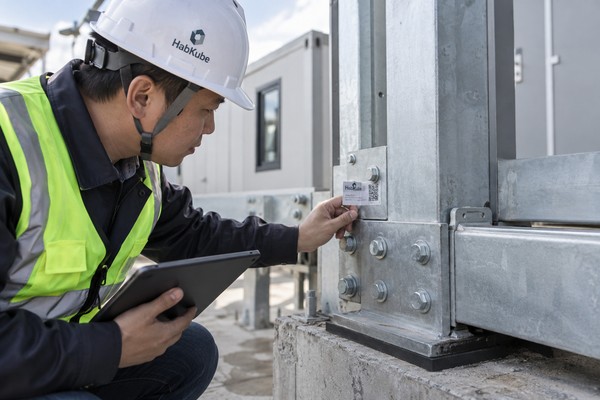
Specify independent evidence without overclaiming it
An implementation check for the buyer
Define what a document proves and what it cannot prove. A product certificate may identify a material, a factory inspection may show the observed assembly, and a shipping document may show that cargo was tendered. None automatically establishes final-site code compliance or full operational performance. Ask who produced each record, what configuration it covers and whether the destination reviewer accepts that evidence. When relying on an external inspector, document sampling basis, access and decision authority before the visit.
Keep exceptions visible through closure. A useful nonconformance record names the affected unit, observed issue, approved correction, reinspection evidence and release decision. Do not hide open items in an email appendix or describe them as “minor” without a criterion. If an unresolved point belongs to local design, keep it outside a supplier’s self-declared pass. The goal is not to block every commercial decision until all uncertainty disappears; it is to put the correct owner and deadline on each uncertainty.
Reconcile the final invoice, packing list, inspection record and receiving report. If a package is damaged, record its identity and condition before contents are dispersed. If a component arrives incomplete, establish whether it was excluded, omitted or lost in transit. That distinction determines the remedy. A repeat buyer can use the first shipment’s exceptions to improve later scopes and inspection points. Treat verified facts as feedback for the next order, not as a reason to invent a success story unsupported by actual project evidence.
Translate the decision into a comparable request for quotation
An implementation check for the buyer
Write an RFQ around the decision in this guide: write a scope that follows the product risks. State the application, destination, intended duration, quantity, site information available and the date by which an approved configuration is needed. Attach one controlled drawing register and name the assumptions that are still open. Ask every bidder to mark each requirement as included, optional, excluded or awaiting buyer input. This is more useful than asking for an all-in figure when the material, factory scope, local work and freight basis may differ. A lower bid can then be traced to an actual difference rather than an unexplained total.
Request a line-item scope for product, finishes, factory checks, export packing, freight, site support and commissioning where relevant. Agree the named delivery place, currency, quotation validity, proposed schedule and change method. Where a calculation or certificate is needed, ask who will provide it and whether it applies to the proposed configuration. A product catalog can help narrow options; it should not be used as the contractual design. The buyer should keep a list of decisions whose late change would affect tooling, dimensions, components or local approval. Put a release owner and deadline beside each one.
Compare supplier answers in a matrix with columns for proposal, evidence, exception, owner and next decision. Record whether an answer is a measured fact, a quoted option, a preliminary assumption or an issue reserved for a destination professional. For prefab house third party inspection, that distinction matters because commercial language can sound final before the site design is ready. Ask the supplier to explain the basis for any performance or delivery claim. The result should be a decision record the purchasing, technical and installation teams can all understand, not an email chain that only its original authors can interpret.
Plan evidence, interfaces and the final handover
An implementation check for the buyer
Make an evidence list for the risks described above, especially insert hold points before concealment. Identify what can be checked at material receipt, during factory production, before shipment and after installation. Those stages do not prove the same things. A visible factory mock-up can confirm geometry and workmanship; it cannot certify a complete building or replace the destination authority. If a report is offered, match its specimen, method, configuration and date to the current order. For each unresolved issue, record the specialist or authority that will decide it and the latest practical decision gate.
Divide responsibility at physical interfaces. Factory-supplied parts, foundations, local structural connections, service terminations, import clearance and occupancy approvals may belong to different parties. Put one owner and one acceptance record beside each interface. Sequence delivery so the site can receive, unload and protect the package safely. Match labels and loose hardware to assembly drawings, and provide receiving staff with dimensions, weights and inspection points before the truck or container arrives. Report transport damage promptly against package IDs while the original condition can still be reconstructed.
At handover, retain approved and as-built drawings, product references, relevant inspection records, operating limits, maintenance instructions and written warranty scope. Link them to actual unit IDs. Identify who can make a later change and when local professional review is needed. Ask the operator to review the building after its first period of use, noting access conflicts, leaks, unexpected wear or service difficulty relevant to this topic. Resolve the underlying cause before duplicating the detail in a later order. This is a practical learning loop, not a claim that a hypothetical example is a delivered HabKube project.
A commercial release gate for this order
An implementation check for the buyer
Before authorizing the next contractual milestone, reconcile the agreed scope, approved changes, inspection status and actual unit IDs. If one document uses a different quantity or revision, resolve it before packing or payment. A practical release is based on identified goods and clear exceptions, not merely a verbal report that the order is “almost done.”
At receipt, compare condition and package identity with the dispatch record. Determine whether open items are supplier corrections, transport claims, local installation work or buyer decisions. Keep the outcome visible to finance and project staff. This final reconciliation closes the commercial loop and gives the next purchase a reliable starting point.
Illustrative project exercise
Use this example to test the decision
Illustrative review: a buyer hires an inspector only after all internal wall services are closed. The inspector can review available records and visible work, but cannot honestly verify every concealed connection. For future units, add a rough-in hold point and define the evidence needed before closure. This example does not imply a defect in any HabKube shipment.
External reference
Use the right reference for the right decision.
Use the approved configuration and destination requirements as the inspection basis; a factory photograph is not a substitute for a reviewed assembly or code approval.
Read ICC off-site fabrication provisionsConclusion
Clarity before commitment.
Third-party inspection is effective when it is early enough, specific enough and tied to a real release decision. Ask for traceable observations and a clear exception process.
Related HabKube resources
Ready when you are
Coordinate an inspection-ready order
Email info@HabKube.com with quantity, configuration and inspection requirements. We can discuss the documents and stages that an independent reviewer will need.
Send your requirementsCommon questions
Before you request a quote.
Does a third-party pass mean the building is code approved?+
No. It means the inspector found the checked items acceptable within its defined assignment. Destination compliance and design approval are separate.
Can one visit cover the whole production?+
A final visit can cover visible items and records, but hidden work may need earlier hold points or other reliable evidence.
Who chooses the inspection checklist?+
The buyer should commission it from the approved design, risks and contract requirements, with technical input from the inspector and supplier.
What should happen after a failed item?+
Record the observation, correction owner, decision authority and reinspection evidence. Do not silently turn a failure into a pass.